Optimized Channel Geometry
Melt distribution channel length is reduced by 25%. This lowers hydraulic resistance within the die and optimizes flow velocity profiles.


SKU: die-head
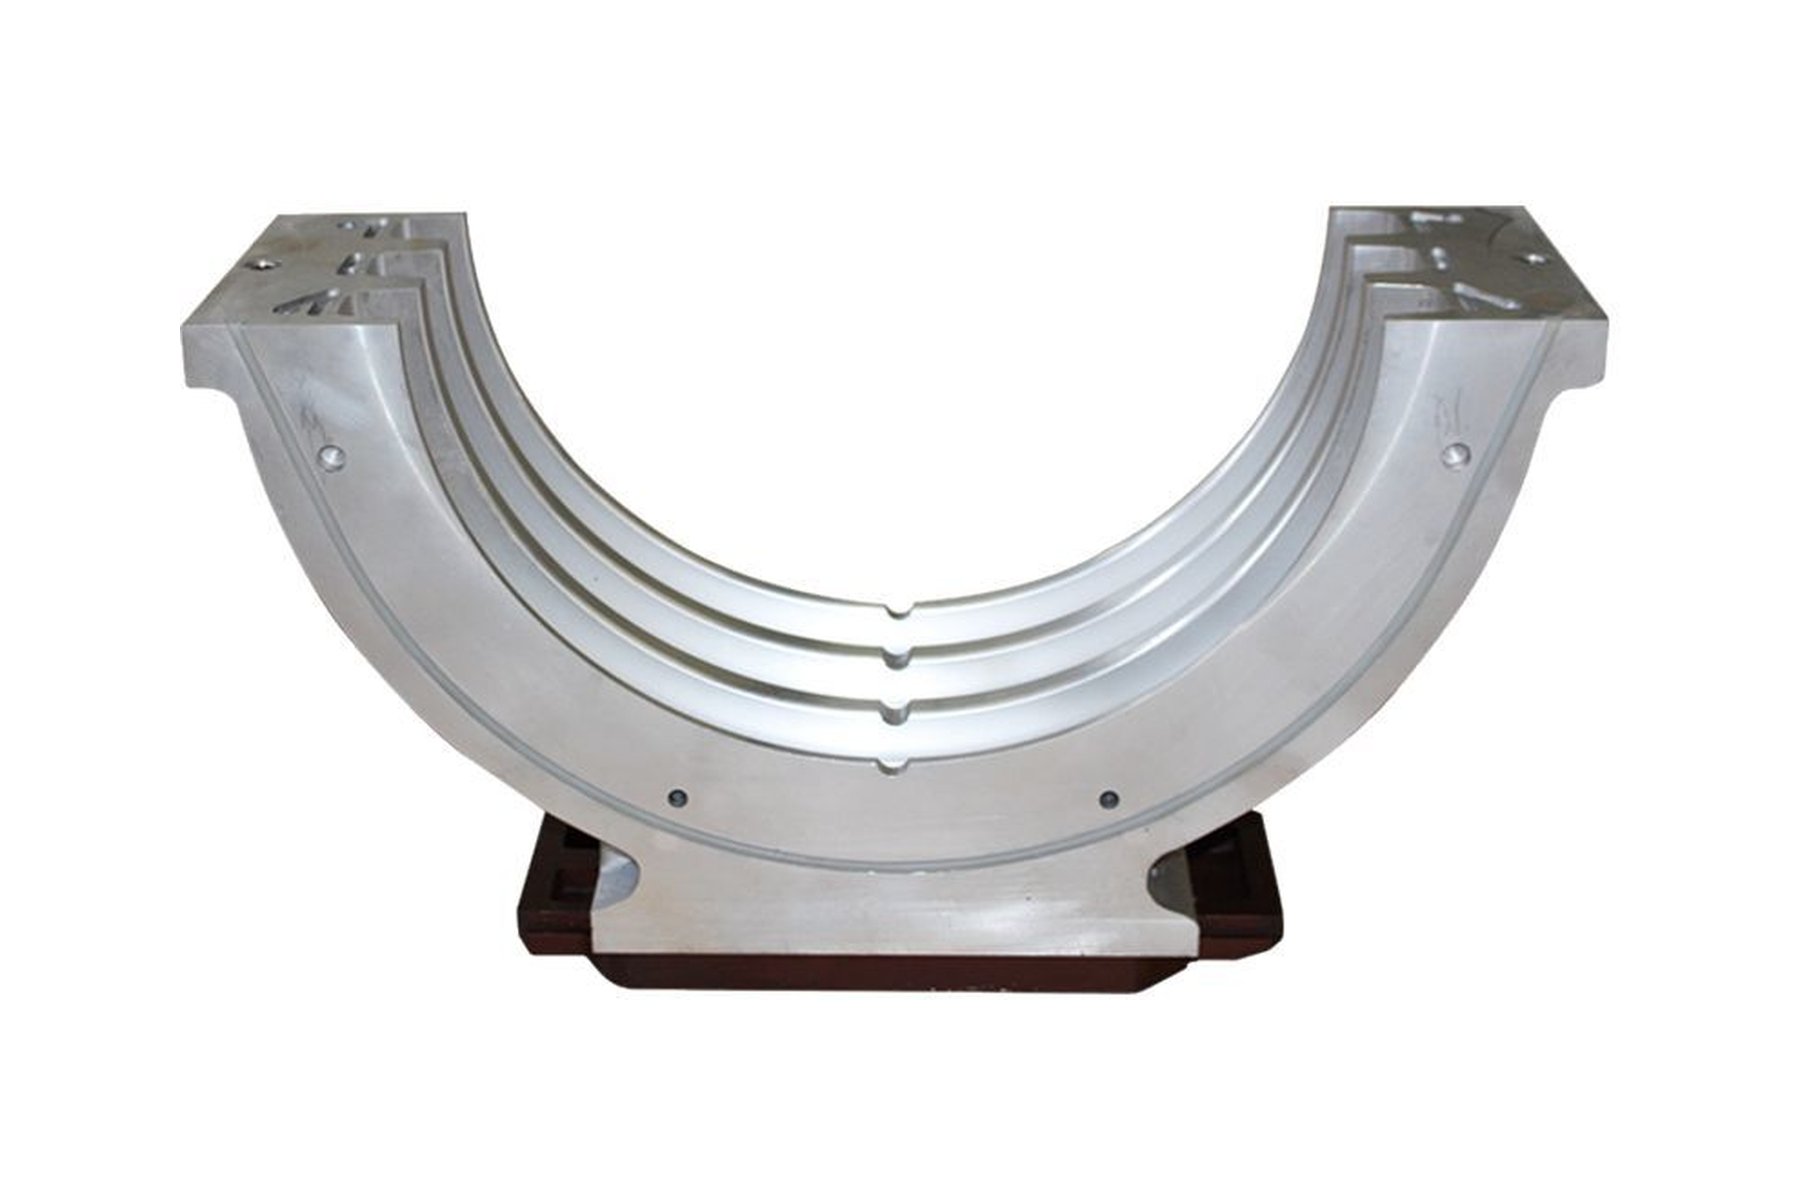
The blank is extruded from the extruder through the inner and outer die of the double layer pipe die head.
Full technical datasheet available
Contact us to receive complete specifications, drawings, and configuration options for your pipe diameter range.
Our specialists will contact you within 24 hours
Advanced technology for reliable production
Melt distribution channel length is reduced by 25%. This lowers hydraulic resistance within the die and optimizes flow velocity profiles.
Processing runs at both lower pressure and reduced melt temperature. This prevents thermal degradation of the polymer and guarantees stable dimensional geometry of the finished product.
Operating under consistently low pressure minimizes seal wear, completely eliminating the risk of joint depressurization and material leakage.
Compared to conventional extrusion dies, the SUBA series delivers a 25% increase in production output using the same facility footprint.
Gentle material processing and reduced die pressure allow the line to operate reliably on a broader range of resin grades, including cost-effective pipe grades and recycled polymers (regrind).
Operating at a lower thermal profile directly cuts energy consumption for both heating and subsequent profile cooling. This minimizes operational expenses (OPEX) and accelerates the return on investment (ROI). The double channel starts from the die head body and reaches the die exit, it achieves multi extruders extrude two layers. Dual-Layer Pipe Dies with Dynamic Adjustment The optimized design of our next-generation dual-layer pipe dies allows for independent adjustment of both the inner and outer wall thicknesses. The core innovation of this unit is the ability to precisely calibrate product geometry directly during the molding process, bringing production flexibility and continuity to a new level.
The upgraded unit allows wall thickness correction directly during extrusion. There is no need to stop the extrusion line to adjust the geometry.
The design eliminates the need to loosen and subsequently tighten fastening bolts when aligning the mandrel and die.
Eliminating repetitive manipulations with the die's fastening elements minimizes wear on mating surfaces and drastically reduces the risk of polymer melt leakage.
On-the-fly adjustment capability completely eradicates forced line stops for wall thickness calibration, maximizing the overall equipment effectiveness (OEE).
Rapid parameter tuning to meet required tolerances cuts the time needed for the line to reach a stable operating mode. Consequently, it sharply reduces startup scrap and material waste.
The extreme simplicity and convenience of the adjustment process ease the operators' workload, lower maintenance labor intensity, and minimize the risk of errors during layer alignment.
Contact us for detailed specifications, pricing, and compatibility information.
essential components for your corrugated pipe production line. Individual upgrades, replacements, and custom configurations available.
Contact us for a free consultation and quote